

Shaanxi Yulin Coal Dust Sealed Conveying Engineering Project
The Yulin area in Shaanxi is an important coal production base in China. The sealed transport of coal dust is a key link in supporting production safety and reducing environmental pollution. A large coal chemical enterprise faced issues such as dust leakage and high material loss during the transfer of raw coal, urgently needing an efficient and environmentally friendly sealed conveying solution. Leveraging its deep experience in pneumatic conveying, Head Powder customized a sealed coal dust conveying project for the company, achieving clean, low-consumption, and stable material transfer.
Customer pain points
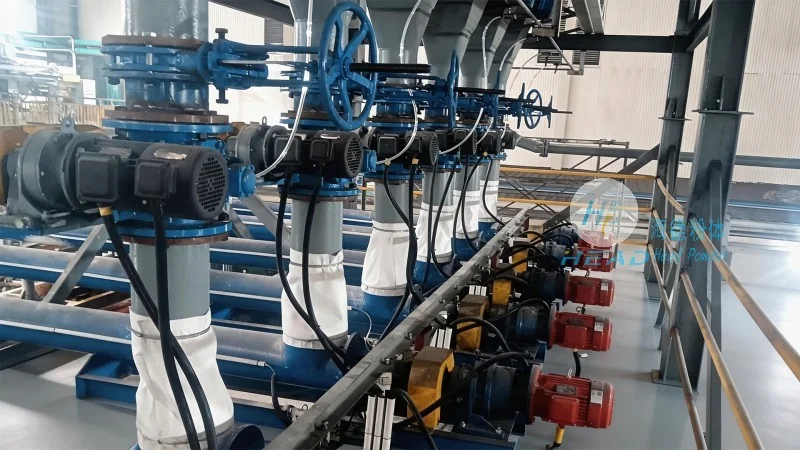
Under the traditional open conveying method, the company faces three major pain points: first, severe coal dust escaping, which not only pollutes the workshop and surrounding environment but also increases occupational health risks for employees; Second, material loss during transportation is significant, and accumulated annual waste can cause significant economic burdens; Third, open conveying poses fire and explosion hazards, putting enormous pressure on safety management. In addition, the failure rate of existing conveyor system equipment is high, and maintenance costs remain high, seriously affecting production continuity.
Product advantages and solutions
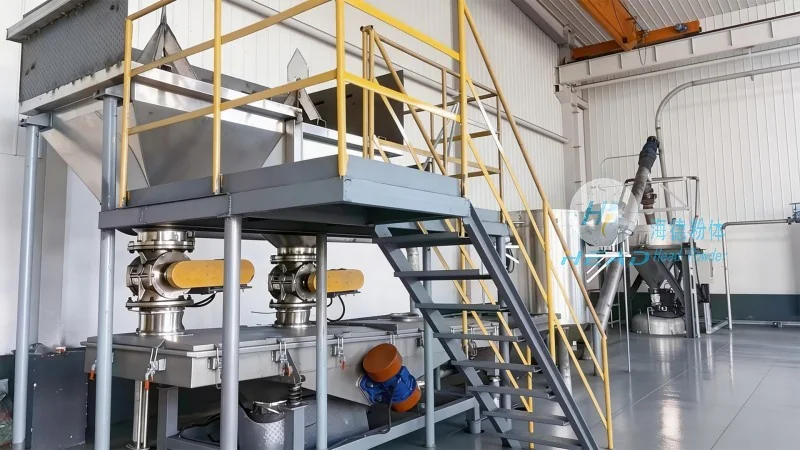
To address these pain points, Head Powder provides a fully enclosed pneumatic conveying system. This system uses a combined negative pressure/positive pressure conveying technology, transporting coal dust directly from the raw material silo through sealed pipelines to the point of use, with no leakage throughout the process. The system is equipped with a high-efficiency dust removal and filtration device to help meet emission standards; At the same time, an intelligent control module is used to monitor pipeline pressure, flow, and material-air ratio in real time, enabling automatic adjustment and fault warning. This solution fundamentally eliminates dust escape, reduces material loss rates to below 0.5%, ensures stable system operation, extends maintenance intervals to over 12 months, and reduces overall operating costs.
Project Results
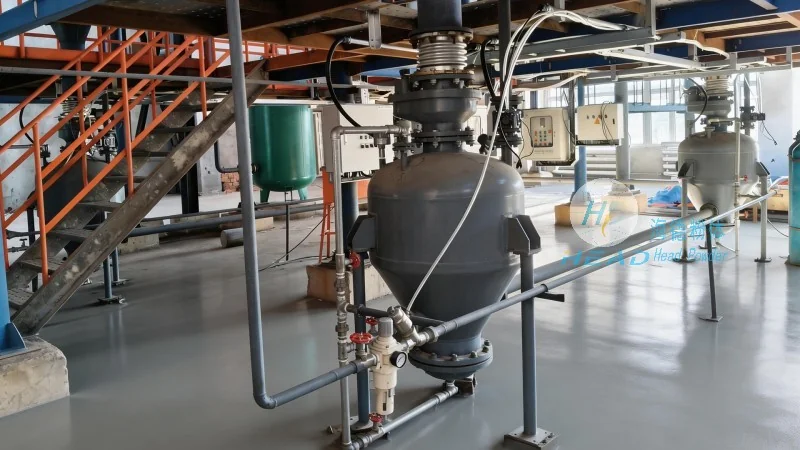
After the project was put into use, the plant's dust concentration in the plant met national occupational health standards, and the environmental emission indicators fully met. Conveying efficiency has increased by 30% compared to the original method, saving over one million yuan in material costs annually. At the same time, the sealed pipelines effectively isolate fire sources from dust contact, thereby enhancing production safety. Head Powder's sealed coal dust conveying solution provides a replicable technical path for handling similar high-dust materials.