

Hunan Changsha Maltodextrin Dust-Free Transportation Complete Project
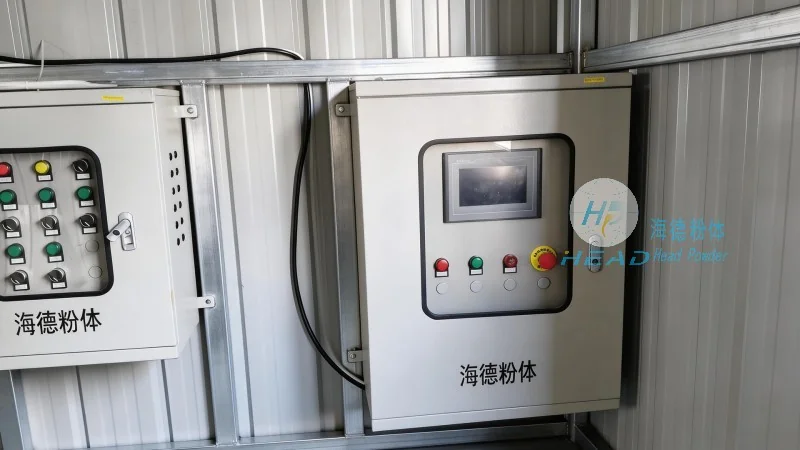
A food manufacturer in Changsha, Hunan, mainly produces high value-added powder raw materials such as maltodextrin. In the traditional production process, powder from feeding and conveying to packaging relied entirely on manual operation and open equipment, resulting in dust spreading and severe material loss. Frequent dust removal consumed a large amount of manpower.
Customer pain points
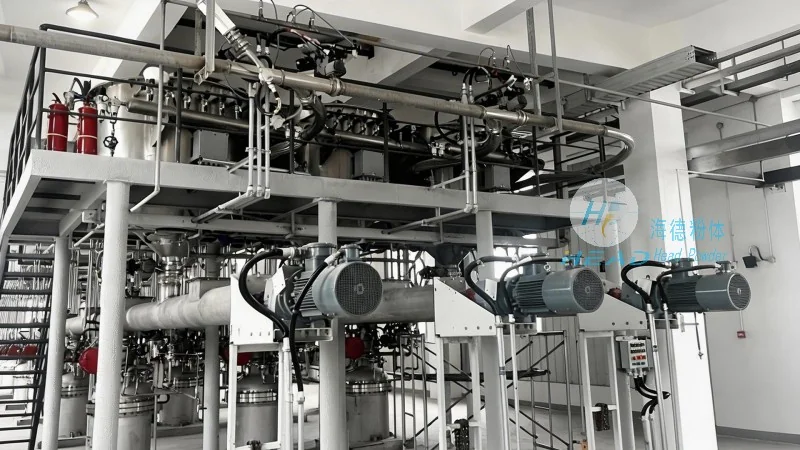
Due to its fine texture and strong hygroscopicity, maltodextrin easily generates dust during traditional transportation, which not only pollutes the workshop environment but also leads to raw material waste rates exceeding 5%. At the same time, dust accumulation carries the usual risk of ignition and explosion, and open conveying methods cannot meet the strict hygiene requirements of the food industry. The customer urgently needed a complete set of equipment that could suppress dust at the source and achieve fully sealed conveying.
Solutions and product advantages
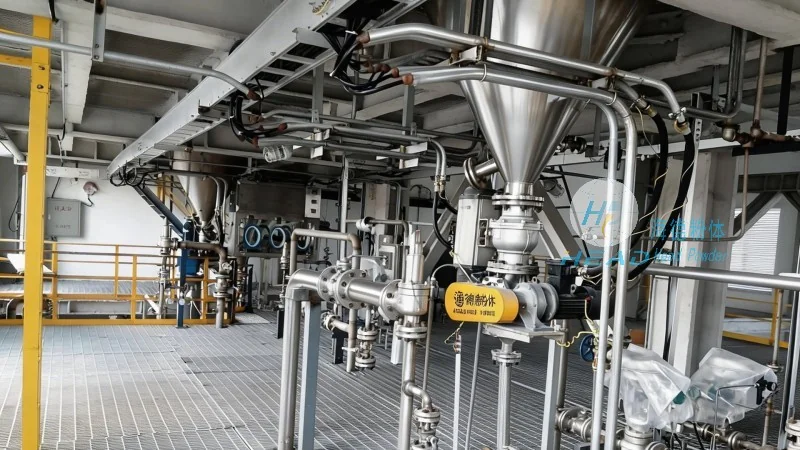
To address these pain points, we designed and implemented a complete dust-free delivery project for maltodextrin. The system uses fully enclosed pipeline pneumatic conveying technology, combined with a high-efficiency pulse reverse blow dust removal device, allowing materials to be transferred within a sealed space, achieving dust-free operation throughout the entire process. The inner walls of the equipment are polished to meet food-grade hygiene standards, and are equipped with an automated control system that intelligently adjusts conveying speed and air pressure according to production needs, reducing manual intervention. After commissioning, workshop dust concentrations dropped below national standards, material losses were controlled within 0.5%, customer production capacity increased by 30%, and overall operating costs dropped by about 15%.