

Liuzhou Sugar Powder Negative Pressure Dust-Free Complete Set
In the powdered sugar processing sector of Liuzhou, Guangxi, a certain company has long faced production challenges such as dust emissions, high material loss, and frequent equipment maintenance. As a high value-added product, powdered sugar not only causes raw material waste during its production but also poses ongoing threats to the workshop environment, employee health, and equipment lifespan. To systematically address this issue, Head Powder has tailored a complete set of powdered sugar negative pressure dust-free projects. Through integrated design, it achieves a fully sealed and automated control process from feeding, conveying, mixing to packaging, effectively eliminating dust spillover, reducing operating costs, and improving production capacity stability.
Customer pain point analysis
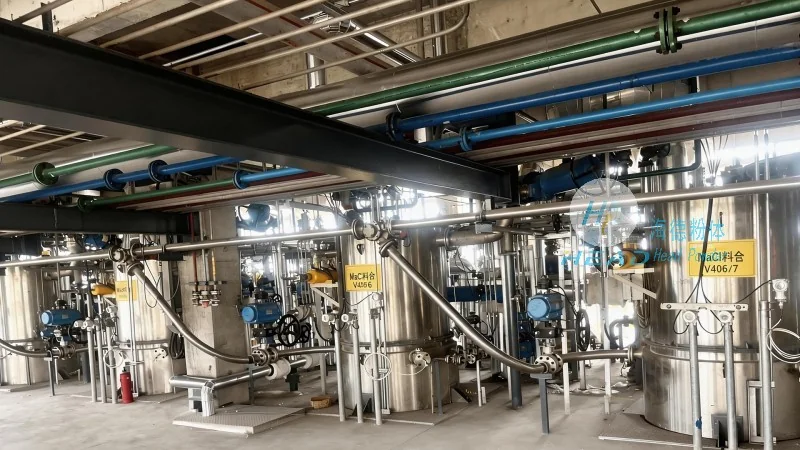
Traditional powdered sugar production lines have the following prominent issues: First, there are many material exposure steps, and processes such as feeding, transportation, and packaging tend to generate large amounts of dust, resulting in low visibility and difficult cleaning in the workshop; Second, open equipment makes powdered sugar prone to moisture and clumping, affecting product quality; Third, high dust concentrations erode electrical equipment and mechanical seals, resulting in high failure rates and long maintenance cycles; Fourth, frequent work not only results in low efficiency but also poses occupational health risks to employees exposed to dust over long periods. These pain points severely restrict companies' capacity utilization and sustainable development.
Head Powder Solutions
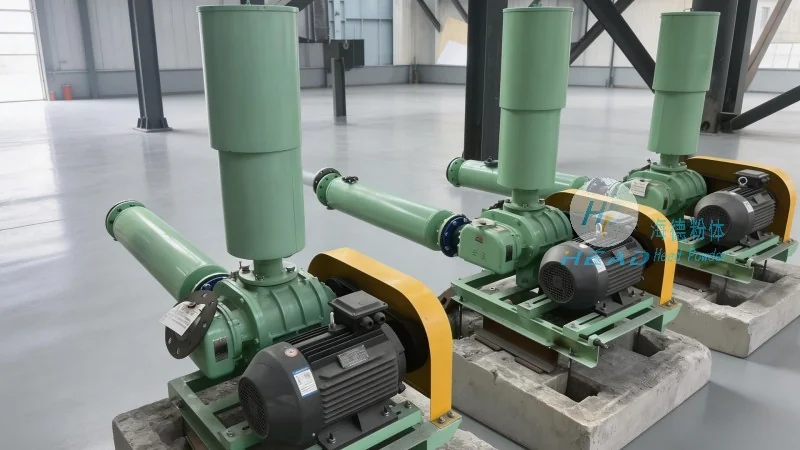
To address these pain points, Head Powder uses negative pressure pneumatic conveying technology as the core, building a complete integrated system of sealed sugar conveying and dust removal. The system uses a negative pressure fan as the power source, drawing powdered sugar from the feeding station to the storage silo through sealed pipelines, then after measurement and mixing, it is conveyed to the packaging machine. All transfer nodes are equipped with pulse reverse blow dust removal devices, helping to prevent dust leakage in the workshop. At the same time, the system is equipped with an intelligent control module that can monitor pipeline pressure, airflow, and material level in real time, automatically adjust operating parameters, and achieve stable unattended operation.
Implementation Effectiveness and Value
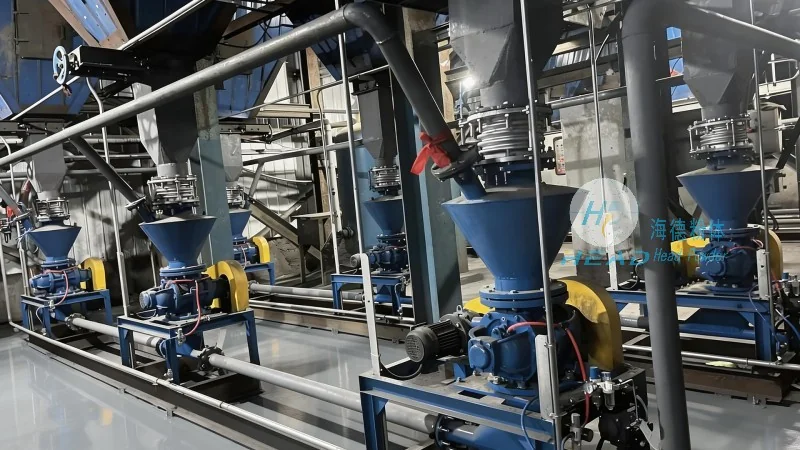
Through this complete project, dust concentrations in the customer's workshop have been reduced below industry standards, and the cleanliness of the site environment has improved; The powder sugar loss rate is about 15% lower than the original process, and material utilization has improved; Equipment maintenance frequency has been reduced from several times a month to once a quarter, and spare parts replacement costs have decreased accordingly. Additionally, the increase in automation reduces the number of operators from the original 8 to 2, effectively alleviating recruitment difficulties. After the project was put into operation, the client's factory met expectations in areas such as clean production, energy conservation and consumption reduction, and safety compliance, setting a benchmark for subsequent production line upgrades.