

Pneumatic conveying solution for quicklime powder
During the transportation and storage of quicklime powder, many companies face issues such as dust pollution, material blockages, low conveying efficiency, and severe equipment wear. Quicklime powder reacts easily when exposed to water, and traditional mechanical conveying methods often cause equipment corrosion and sealing failure, thereby increasing maintenance costs and downtime. In addition, manual handling or simple pneumatic conveying systems are difficult to achieve precise control, leading to material waste and harsh working environments, affecting overall production efficiency.
Material Characteristic Analysis
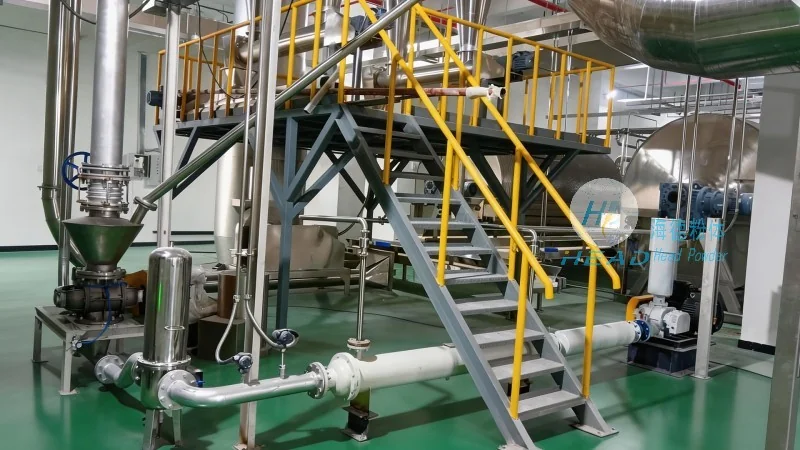
Quicklime powder (mainly composed of calcium oxide) is a powder material with high fineness, low specific gravity, poor flowability, and strong hygroscopicity. Their particle size usually ranges from several tens to several hundred microns, making them prone to dust in the air. When exposed to water or humid environments, they rapidly undergo chemical reactions, releasing heat and clumping. Therefore, it is recommended that the conveying system have good sealing, moisture resistance, and wear resistance to prevent material deterioration and equipment failure.
Head Powder Quicklime Pneumatic Conveying System
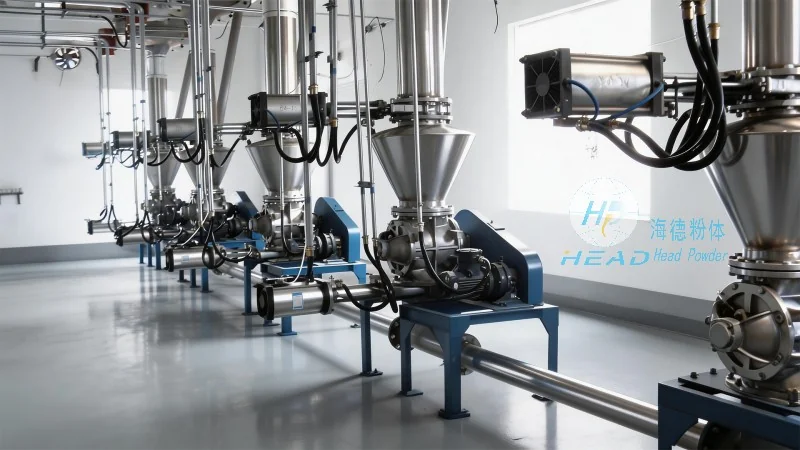
Head Powder offers customized pneumatic conveying solutions tailored to the special properties of quicklime powder. The system uses positive or negative pressure conveying methods, efficiently transporting quicklime powder from the feeding point to storage or usage areas through sealed pipelines. Core equipment includes dedicated transmitters, high-efficiency separators, pulse dust collectors, and intelligent control systems, which help ensure stable and leak-free conveying processes and adapt to process requirements at different distances and heights. The conveyor system is made of corrosion-resistant and wear-resistant materials, extending equipment service life while reducing maintenance frequency.
Solutions and core values
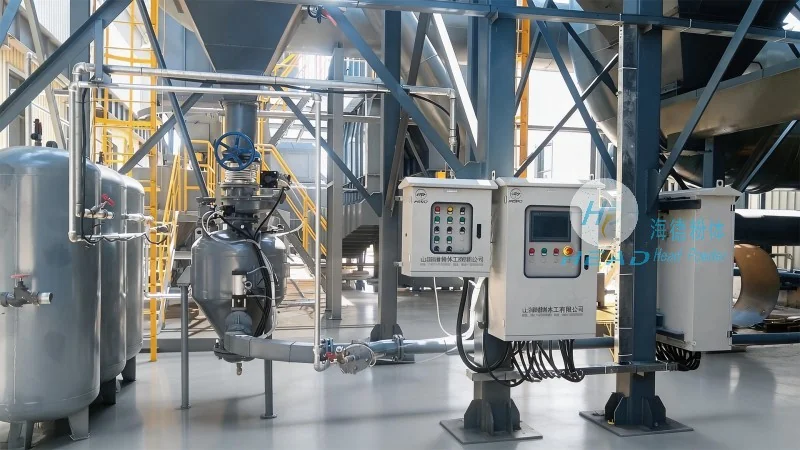
To address common issues of material blockages and dust pollution among customers, Head Powder has introduced fluidization technology and airflow regulation devices into its system design, effectively improving the flow and continuity of quicklime powder. Through sealed structural design and efficient dust removal equipment, dust concentration in the working environment is kept within safety standards, protecting operator health. The intelligent control system can monitor conveying pressure, flow, and material level in real time, enabling automated operation and fault warning, reducing manual intervention and improving production efficiency. Additionally, the system can be modularly customized according to customers' actual working conditions (such as conveying distance, height, and conveying volume), flexibly adapting to site layouts and reducing overall operating costs.