

Pneumatic conveying solution for plastic food carrier pellets
In the production line transfer of plastic food carrier particles (such as bottle caps, trays, packaging containers, etc.), traditional mechanical conveying often faces challenges such as fragile materials, dust dispersion, restricted paths, and cleaning difficulties. Debris and dust not only affect product quality but also increase equipment wear and labor cleaning costs; Fixed mechanical conveyor belts struggle to adapt to the flexible layout of multiple types and blanking points, resulting in long production line renovation cycles and high investment. In addition, food-grade materials have strict hygiene requirements during transportation, and ordinary mechanical structures are prone to contamination and dirt, which cannot meet HACCP and other system certification requirements.
Material characteristics: lightweight, fragile, irregular, hygienically sensitive
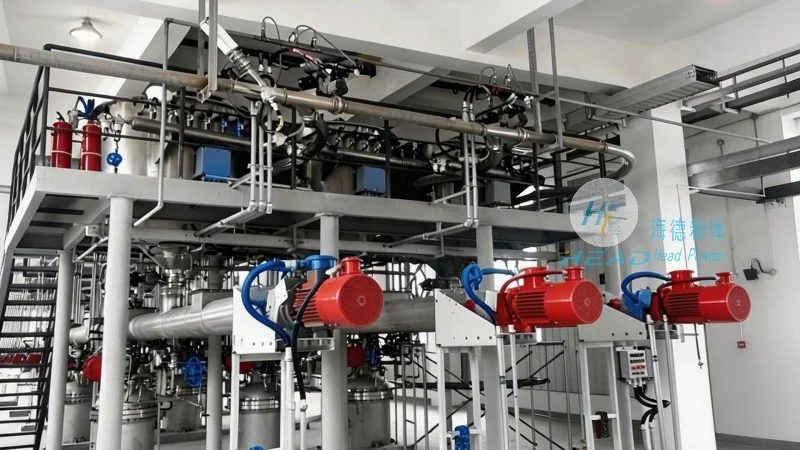
Plastic food carriers have low particle density (0.1–0.6 g/cm³), diverse shapes (bottle caps, knives, forks, trays, etc.), smooth surfaces, and high brittleness. Some materials carry static electricity or oil stains, which easily adhere to or adhere to the pipe wall. At the same time, as packaging materials that come into direct contact with food, it is recommended to prevent secondary contamination during transportation, avoid foreign matter contamination, and achieve rapid production change without residue.
Product Introduction: Head powder plastic food carrier particle pneumatic conveying system
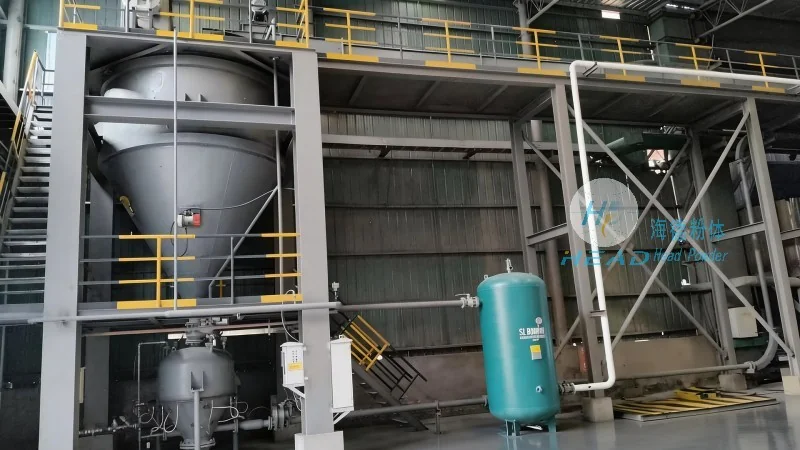
Head Powder addresses these pain points by offering customized pneumatic conveying solutions. The system uses positive pressure dilute phase or dense phase conveying methods, using closed pipelines to accurately transport plastic carrier pellets from storage silos, unpacking stations, injection molding machine discharge ports, and other sources to packaging machines, assembly stations, or storage areas. Key equipment includes venturi feeders, rotary valves, directional valves, cyclone separators, and automatic back-blow dust removal devices. The inner walls of the pipes are mirror-polished, and all contact parts comply with food contact material standards (such as FDA or EU 10/2011).
Product Advantages: Targeted solutions
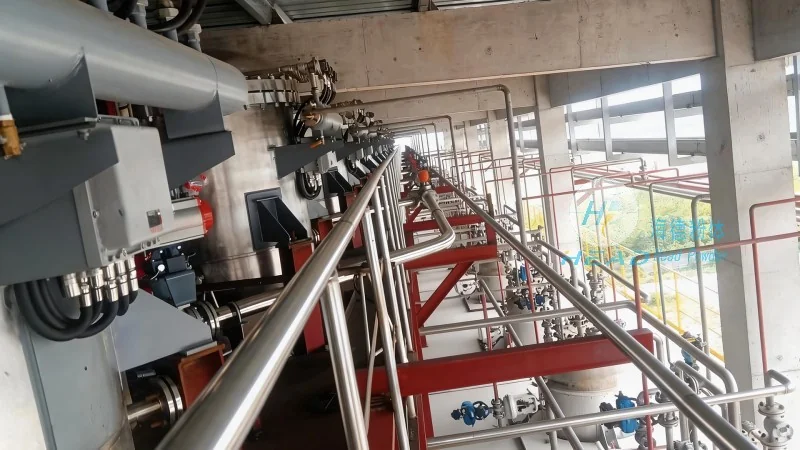
1. Low breakage, dust-free: Optimize airflow velocity and pipe elbow radius, with material collision and pipe wall friction below 0.3%; Fully enclosed negative pressure/positive pressure operation reduces workshop dust concentration below 1 mg/m³.
2. Flexible layout and easy expansion: Pipelines can be routed along walls and ceilings, easily bypassing equipment and columns, and supports automatic switching between multiple cutting points; The new workstation only requires adding valves and branch pipelines, without stopping for modifications.
3. Hygienic and easy to clean: The system is equipped with a quick-release purification chamber, an online cleaning interface (CIP), and detachable seals; Material residue rate is below 0.05%, and production change takes only 15 minutes.
4. Intelligent control reduces operation and maintenance:P LC+HMI centrally monitors parameters such as conveying pressure, flow, and motor load, automatically adjusting the air replenishment volume; The warning module provides early warnings of pipeline blockages or filter saturation, reducing downtime rates by 70%.
Head Powder has over 18 years of hands-on experience in pneumatic conveying, providing one-stop turnkey services from material testing and piping design to electrical integration. Currently, this solution has been successfully applied in many food packaging companies, disposable tableware manufacturers, and beverage bottle cap factories, helping customers reduce manual handling costs by 30% on average and improve overall production line efficiency by 20%.