

Low-crushing sugar powder conveying system in Nanchang, Jiangxi
A food manufacturing company located in Nanchang, Jiangxi, mainly produces various powdered sugar products. During the long-term production process, the delivery of powdered sugar has always been a technical challenge for the company. Because powdered sugar is fine and brittle, traditional conveying equipment tends to cause large amounts of crushing during transportation, leading to a decline in product quality and dust buildup. This not only increases material waste but also affects the production environment and employee health. To address this pain point, Head Powder customized a low-crushing sugar powder conveying system for the company, improving the breakage and dust issues during transportation.
Customer pain points
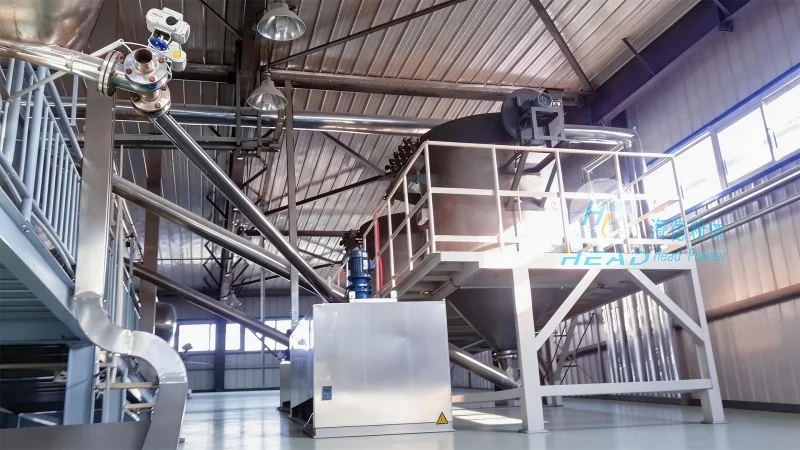
Customers face the following core challenges in the powdered sugar conveying process:
- During transportation, powdered sugar granules are subjected to mechanical impact and friction, resulting in a breakage rate of over 15%, which directly leads to substandard product particle size and affects both price and customer satisfaction.
- Dust overflow causes air pollution in workshops, with annual material losses of about 3%~5%, while also increasing cleaning costs and pressure to meet environmental protection standards.
- Traditional conveying equipment consumes high energy and frequently experiences blockages and wear, with long maintenance downtime and affecting capacity continuity.
Solutions and product advantages
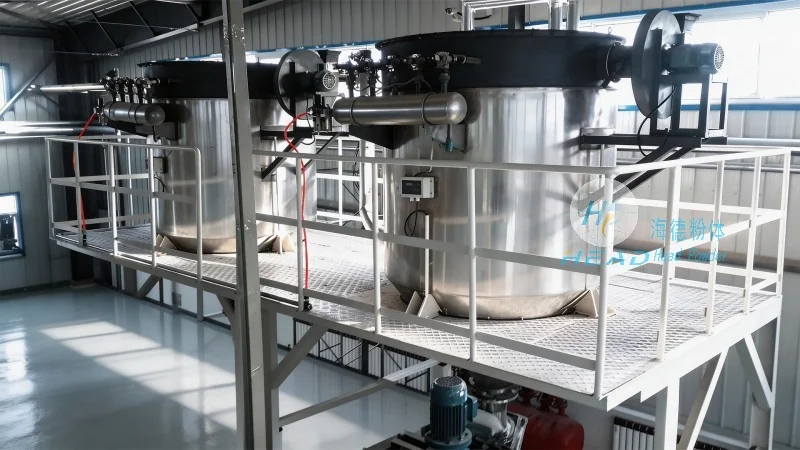
The low-crushing sugar powder conveying system provided by Head Powder has been specially optimized to address the above issues:
- Low Crush Design:By using flexible conveying pipelines and a specially structured pneumatic conveying system, materials move within the pipeline at low speed and with low impact. The crushing rate of sugar powder can be controlled within 2%, significantly preserving the integrity of the particles.
- Airtight and dust-free:Fully enclosed conveyor pipelines combined with high-efficiency dust removal devices ensure zero dust leakage, ensuring workshop cleanliness meets food production requirements while reducing material loss.
- Energy saving and high efficiency:Optimizing air source matching and pipeline layout, system operating energy consumption is reduced by about 20% compared to traditional solutions, and conveying efficiency is increased by more than 30%.
- Intelligent Control:Equipped with an online monitoring and automatic adjustment system, it can monitor conveying pressure, flow, and crushing status in real time, supports remote operation and maintenance, and reduces manual intervention and maintenance frequency.
After successfully applying this system on the customer's production line, the crushing rate of powdered sugar dropped significantly, product quality stabilized, workshop dust concentration was below national standards, and annual material and maintenance savings exceeded hundreds of thousands of yuan, earning high recognition from the customer.