

Dust-free sealed conveying system for hazardous powder in Yichun, Jiangxi
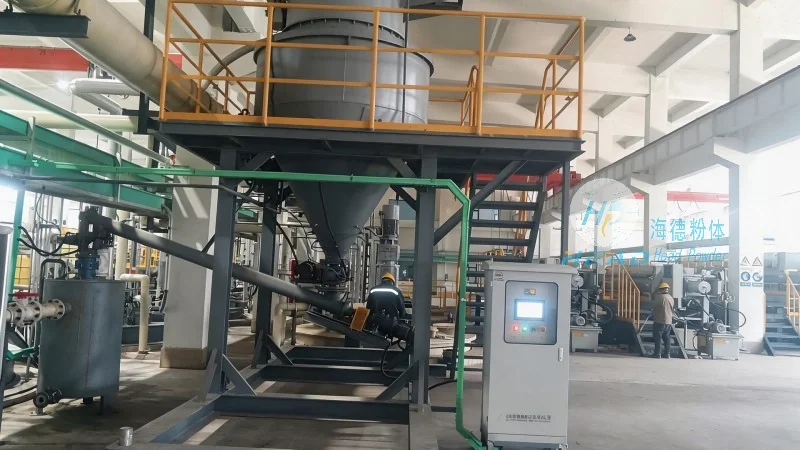
A hazardous waste treatment enterprise in Yichun, Jiangxi, mainly engaged in the resource utilization of non-ferrous metal smelting waste slag and chemical waste. During production, various hazardous waste powders (such as incineration fly ash containing heavy metals, desulfurized gypsum powder, etc.) need to be transported from the temporary storage warehouse to the batching system. Due to the complex nature of the materials (high humidity, strong corrosiveness, and easy dust generation), the original open conveying method led to widespread dust on site, severe equipment corrosion, and occupational health risks for personnel. After extensive research, the company ultimately chose Head Powder's dust-free sealed conveying system to achieve fully sealed and automated operation of powder from feeding to feeding.
Customer pain points
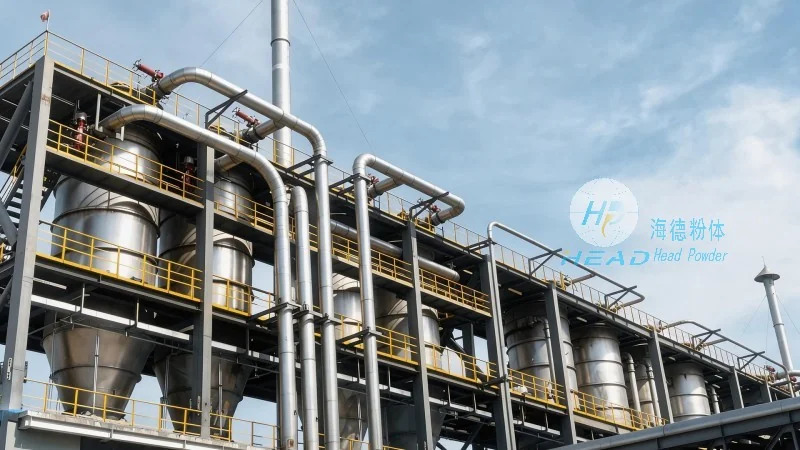
1. Severe dust pollution: Traditional belt or screw conveyors cannot be properly sealed, powder leakage rates exceed 5%, workshop PM2.5 concentrations have long exceeded standards, and environmental inspections require frequent rectification.
2. High equipment failure rate: Corrosive dust enters bearings, motors, and other components, requiring sealing replacements every quarter, with annual maintenance costs accounting for 18% of equipment costs.
3. Material waste and cross-contamination: Powder scattering during transportation causes raw material loss, and different batches of materials often face mixing risks, affecting downstream process stability.
4. High dependence on manual labor: Requires dedicated personnel to clean dust and inspect leaks, and workers must wear full protective equipment, resulting in low operational efficiency and safety hazards.
Product advantages
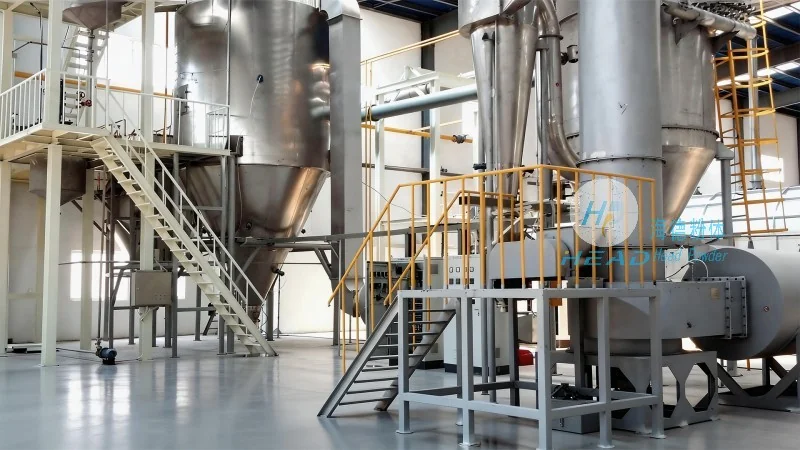
To address these pain points, Head Powder customized a dust-free sealed conveying system for hazardous waste powder for the company. The main features are as follows:
Fully enclosed pipeline transportation: Uses stainless steel seamless pipes and highly airtight rotary feed valves, with a system leakage rate below 0.01%, preventing dust leakage from the source. The inner wall of the pipeline is specially mirror-treated, with a material residue rate less than 0.05kg/m³, effectively preventing cross-contamination.
Negative or positive pressure is more accurately controlled: Matched pneumatic conveying mode (dilute/dense phase) according to material characteristics, equipped with variable frequency Roots fans and intelligent pressure regulating valves, stable and adjustable conveying speed, allowing lumped materials with a maximum particle size of 50mm to pass smoothly without pipeline blockages.
Intelligent monitoring and self-cleaning: Integrates online dust concentration detection, pipeline pressure monitoring, and material level alarm system. If an abnormality is detected, it automatically shuts down and triggers a pulse backflow device to help the system run continuously. The operation interface is fully touch-enabled, recording conveying volume and energy consumption data for each batch.
Modular quick-assembly structure: All components use flange connections and quick-install clamps, reducing on-site installation time by 60% compared to traditional methods. Reserved expansion interfaces allow easy integration of new production lines in the future. The overall explosion-proof rating of the system reaches ExdII.BT4, meeting the explosion-proof requirements of hazardous waste workshops.