

Shanxi Linfen Waste Incineration Powder Sealed Conveying Project
The Shanxi Linfen Waste Incineration Powder Sealed Conveyance Project is a systematic solution for efficient, environmentally friendly, and safe conveying of powdered materials (such as fly ash, limestone powder, etc.) generated during the waste incineration power generation process. The project adopts Head Powder's independently developed sealed conveying technology, improving issues such as dust leakage, material loss, and secondary environmental pollution caused by traditional conveying methods, helping waste-to-energy power plants achieve clean production and resource utilization.
Project Background and Client Pain Points
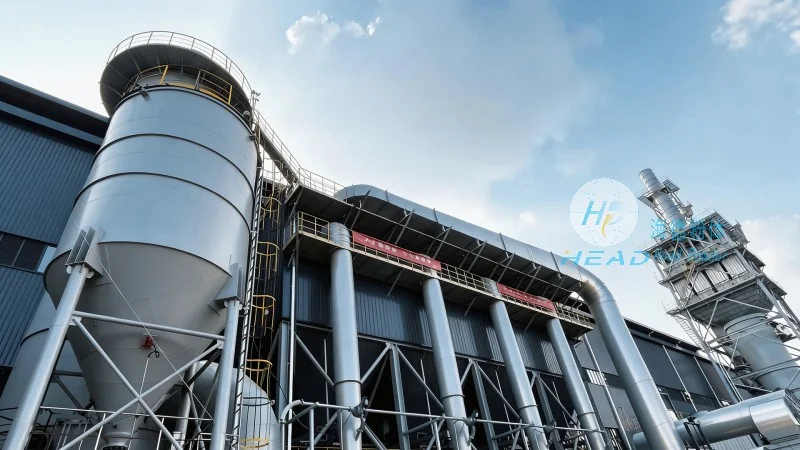
In the waste-to-energy incineration power generation process, the transportation of powdered materials is a crucial step. Customers face the following core pain points:
- Severe dust pollution: Traditional open conveying causes large amounts of dust to escape, affecting the factory environment and employee health, and making it difficult to meet increasingly stringent environmental emission standards.
- Material loss and waste: During transportation, materials are lost due to leaks, moisture, or caking, increasing operating costs.
- Frequent equipment maintenance: Mechanical components such as chains and belts are prone to wear, with high failure rates; downtime for maintenance affects production continuity.
- Low level of automation: There are many manual operation steps, making real-time monitoring of conveying status impossible, making material blockages and cutoffs common.
Solutions and product advantages
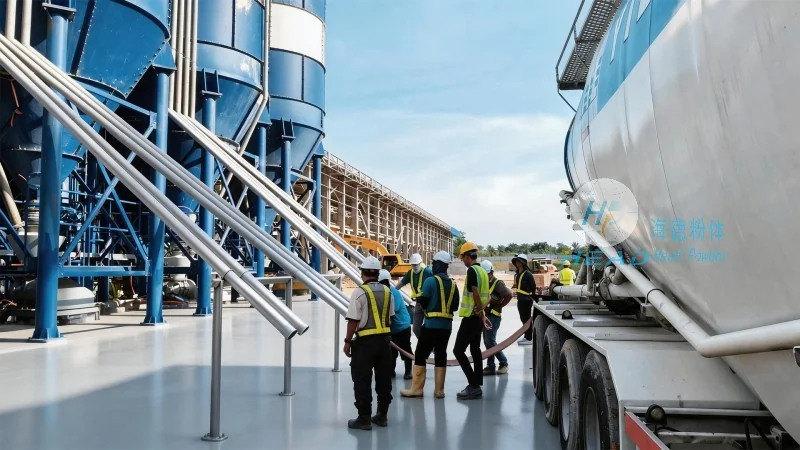
To address these pain points, Head Powder offers a complete set of sealed conveying system solutions, with specific advantages including:
- Fully enclosed negative pressure conveying: Uses a combination of pneumatic conveying and mechanical sealing technology, with the system operating under negative or slightly positive pressure throughout the process, zero dust leakage, and meeting lower emission requirements.
- Low energy consumption and high efficiency: Optimized pipeline layout and air source matching, saving over 15% energy compared to traditional equipment, stable conveying capacity, suitable for long-distance, multi-curve conditions.
- Intelligent control: Integrates PLC automatic control system and online monitoring module, providing real-time feedback on flow, pressure, temperature, and other parameters, supporting remote operation and maintenance and fault warning, reducing manual intervention.
- Durable and easy to maintain: Key components use wear-resistant materials combined with quick-release design, making daily maintenance simple, having a long service life, and significantly reducing overall operation and maintenance costs.
Currently, the project has been successfully put into operation, with the system running smoothly, dust emission concentration below 5mg/m³, and material conveying efficiency improved by more than 30%, earning high recognition from customers. The project provides a reliable technical demonstration for sealed powder transportation in the waste incineration industry.