

Negative pressure dilute phase starch system in Hohhot, Inner Mongolia
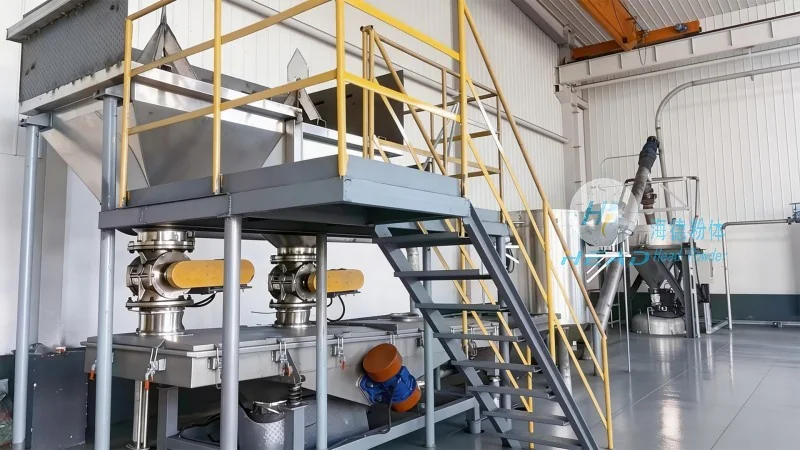
At a starch processing company in Hohhot, Inner Mongolia, the production process requires transporting starch raw materials from the storage area to the production workshop. Traditional conveying methods suffer from dust leakage, high energy consumption, and frequent equipment maintenance, directly affecting the workshop environment and production efficiency. Head Powder has tailored a starch negative pressure dilute phase conveying system for such scenarios, addressing multiple challenges in material handling.
Customer pain points
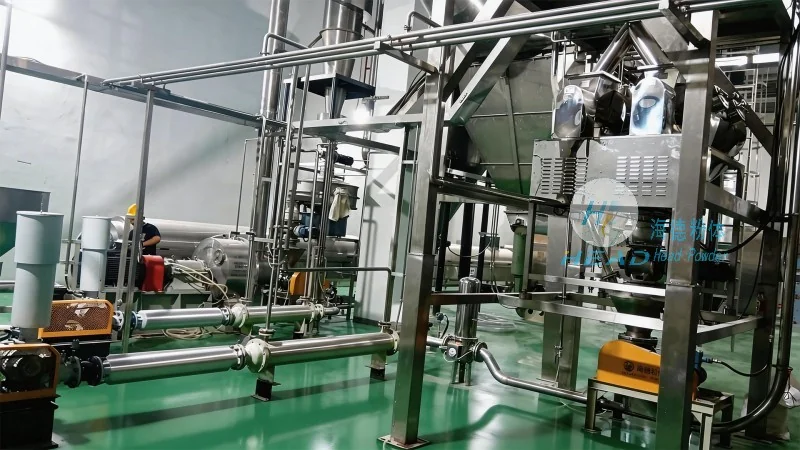
Enterprises face the following challenges in starch transportation: First, starch dust is fine and easily dispersed, causing poor air quality in workshops, affecting employee health, and increasing cleaning costs; Second, traditional mechanical conveying equipment wears out quickly, has short maintenance cycles, and frequent shutdowns affect continuous production; Third, unstable conveying efficiency, high energy consumption, and difficulty controlling operating costs; Fourth, spatial layout is limited, and existing equipment cannot meet the needs of process transformation.
Solution
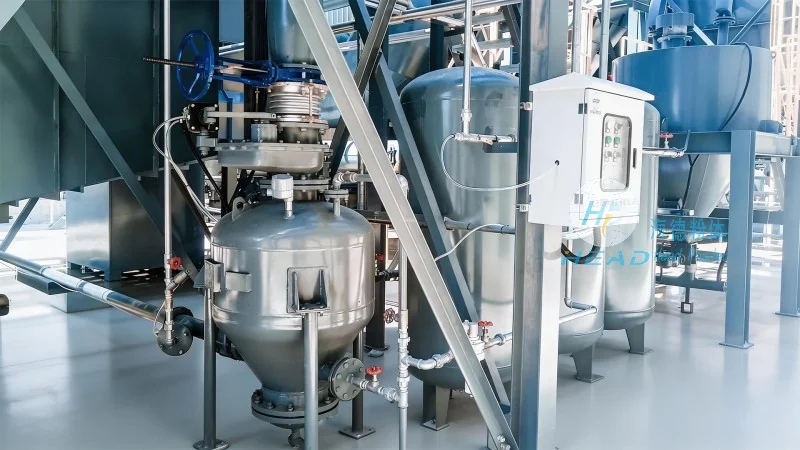
The negative pressure dilute phase conveying system provided by Head Powder uses a sealed pipeline negative pressure suction method to stably transport starch from the feeding point to multiple target stations. The system is equipped with a high-efficiency filtration device to achieve dust-free operations and improve the workshop environment; Wear-resistant pipelines and low-speed fans are used to reduce equipment wear and extend service life; By adjusting the conveying speed and gas-solid ratio via an intelligent control module, energy consumption is reduced while improving the conveying volume; The modular design facilitates flexible layout, adapting to different factory spatial conditions.
After the system was put into operation, dust concentration in the enterprise workshop dropped significantly, equipment maintenance frequency dropped from once a month to once a quarter, energy consumption during conveying was reduced by about 20%, and overall operational stability was recognized by customers. Head Powder continuously provides technical and spare parts support, helping the system operate at high efficiency over the long term.