

Pneumatic conveying solution for magnesium oxide powder
In the industrial application of magnesium oxide powder, achieving efficient, clean, and stable material transportation has always been a key and challenging issue in production management. Based on years of powder engineering experience, Head Powder provides comprehensive customized pneumatic conveying solutions and system equipment tailored to the special properties of magnesium oxide powder, helping enterprises solve various challenges during the conveying process.
Customer pain points
Magnesium oxide powder often faces severe dust pollution, frequent pipeline blockages, low conveying efficiency, and rapid equipment wear during traditional transportation. Especially for fine powder materials, poor sealing leads to increased raw material waste and worsening working conditions, while instability in the conveying system can also affect subsequent process continuity and product quality.
Material characteristics
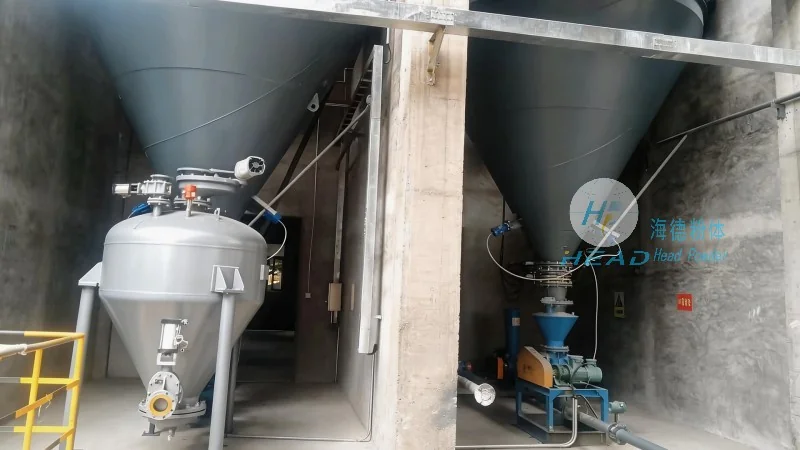
Magnesium oxide powder has the following typical physical properties: fine particle size (usually 200 mesh to 325 mesh), medium density (bulk density about 0.5~0.8 g/cm³), prone to moisture absorption and caking, average fluidity, and generally abrasive. These characteristics require the conveying system to be sealed, moisture-proof, clogged, wear-resistant, and have adjustable flow rate.
Product Introduction
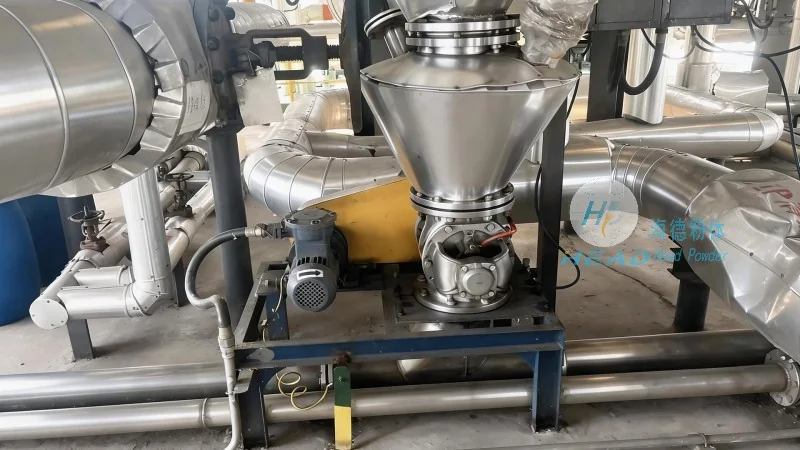
The magnesium oxide pneumatic conveying system provided by Head Powder uses either positive or negative pressure dense or dilute phase conveying methods, and is customized non-standard according to customer site conditions and material characteristics. The system includes feeding devices (such as rotary feeders and venturi feeders), conveying pipelines, air source equipment (fans or compressed air systems), gas-solid separation devices (cyclone separators, baghouse dust collectors), and automatic control units, achieving fully enclosed and automated operation.
Product advantages
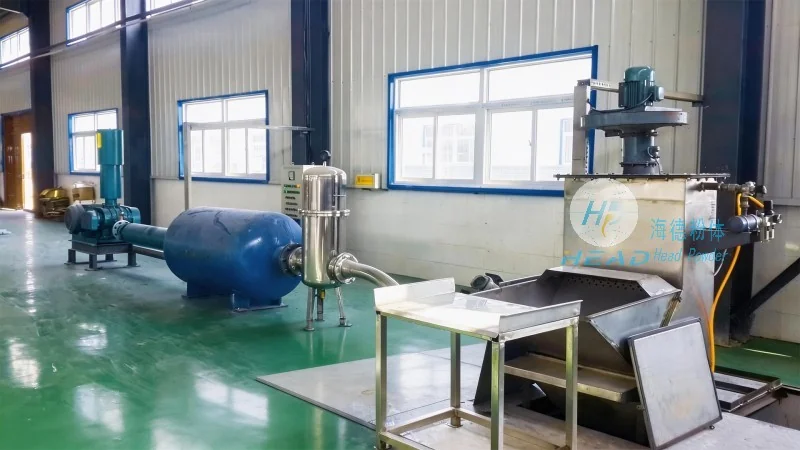
To address customer pain points, Head Powder has implemented multiple targeted designs in its magnesium oxide powder pneumatic conveying solution: a fully enclosed pipeline system to prevent dust leakage; Added moisture-proof and anti-blockage mechanisms to reduce pipe wall adhesion caused by moisture absorption; The inner walls of the pipes are treated with wear resistance to extend their service life; The air-to-material ratio is adjusted through an intelligent control module to accommodate different conveying distances and production capacity requirements. Ultimately, dust-free operations, low-energy consumption, and highly stable conveying are achieved.