

Pneumatic conveying solution for phosphor powder
During the production and application of phosphors, traditional conveying methods often face problems such as dust flying, material moisture and clumping, low conveying efficiency, and rapid equipment wear. Especially since phosphor particles are fine and have low density, direct exposure to air not only causes waste but also affects the environment and operator health. At the same time, consistency between batches is hard to contribute, and manual handling increases labor costs—these pain points are forcing the industry to seek more efficient and cleaner delivery methods.
Material properties: The physical and chemical characteristics of the phosphor
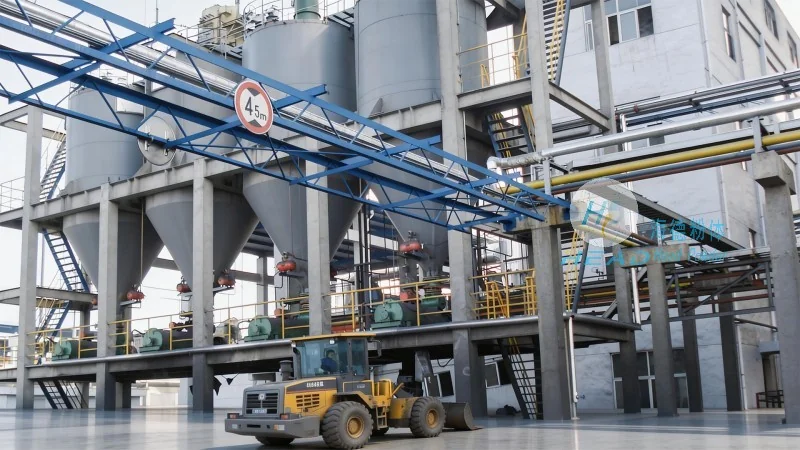
Phosphors are usually micron-level powders, with fine particles, average flowability, and sensitivity to humidity. Its density is mostly between 1.0-3.0 g/cm³, and some varieties are prone to static electricity and have typical moisture absorption. Therefore, the conveying system must fully consider moisture-proofing, anti-static, dust-proof, and material breakage requirements to help ensure stable material transport in a sealed environment, maintaining original purity and luminescence performance.
Product Introduction: Head Pneumatic Conveying System for Powder and Phosphors
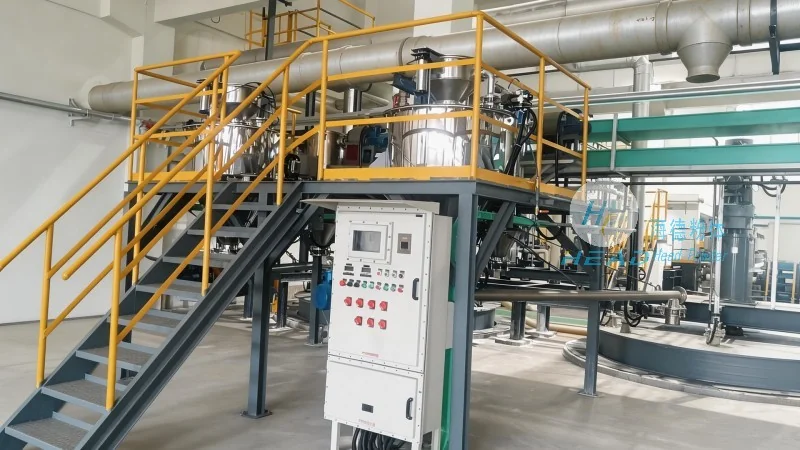
Head Powder offers customized pneumatic conveying solutions and complete equipment tailored to the unique properties of phosphors. The system uses positive or negative pressure dense phase conveying methods, transporting phosphors from the feeding point to downstream processes in a sealed pipeline. Core equipment includes rotary feeders, silo pumps, dust removal and filtration devices, automatic control systems, etc. Non-standard designs can be made according to customer production capacity, workshop layout, and material characteristics to achieve dust-free, automated, and continuous material transportation.
Product Advantages: Targeted solutions to customers' core pain points
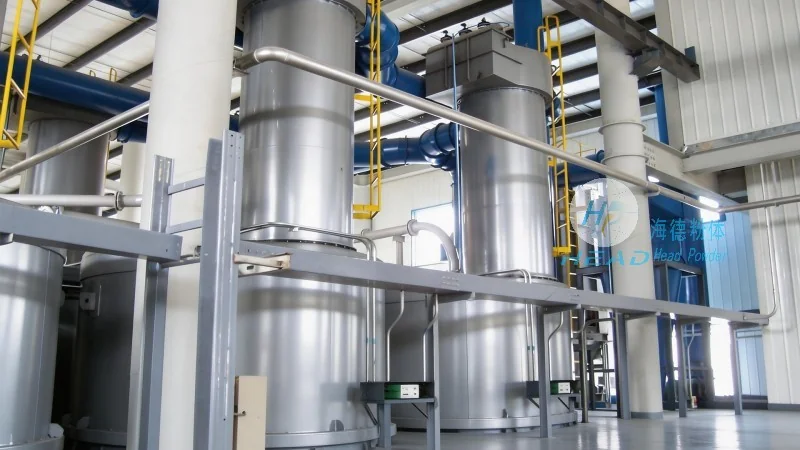
- Sealed tightly and free of dust: The entire system pipeline is sealed, combined with a high-efficiency dust removal device to prevent dust leakage at the source, improve the working environment, and reduce material waste.
- Moisture-proof and anti-clumping: The airflow is dehumidified, keeping the pipeline dry inside; At the same time, a silo temperature and humidity monitoring system is provided to prevent phosphor from absorbing moisture and deteriorating.
- Low breakage rate: Uses low-speed dense phase or bolt-flow conveying technology; materials are specially lined at elbows and valves to greatly reduce particle damage and support product quality.
- Intelligent customization: Integrated PLC automatic control, supports recipe management, remote monitoring, and fault alarms; It can flexibly match conveying pressure, air volume, and path according to actual working conditions to suit different project requirements.