

Pneumatic conveying solution for phosphate ore powder
During the processing and utilization of phosphate ore powder, traditional transportation methods often face many challenges: dust emissions leading to environmental degradation and material loss, frequent pipeline blockages leading to work stoppages for maintenance, severe wear on high-hardness particles that severely shorten equipment lifespan, persistently high energy consumption, and continuously rising operation and maintenance costs. How to achieve efficient, clean, and low-consumption continuous conveying has become a bottleneck that many phosphorus chemical enterprises urgently need to overcome.
Analysis of phosphate ore powder material characteristics
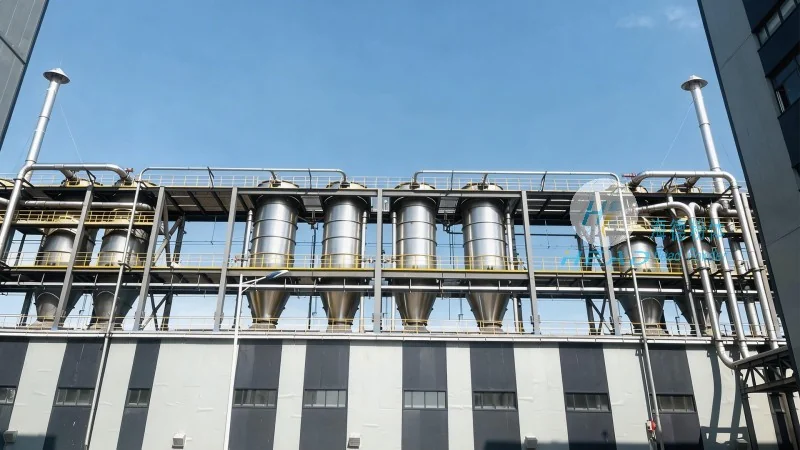
Phosphate ore powder is a finely powdered mineral raw material, with a density typically between 1.4~1.8 t/m³ and a wide particle size distribution (ranging from tens to hundreds of microns). Its particles are typically abrasive and prone to moisture absorption and caking. During conveying, if the airflow speed or pipeline design is improper, settlement, wall slitting, or even blockage can easily occur. In addition, the flowability of phosphate powder is significantly affected by moisture, so special attention must be paid to sealing and moisture-proof design. These characteristics determine that the conveyor system should balance wear resistance, sealing, and adaptability to working conditions.
Introduction to the phosphate powder pneumatic conveying system
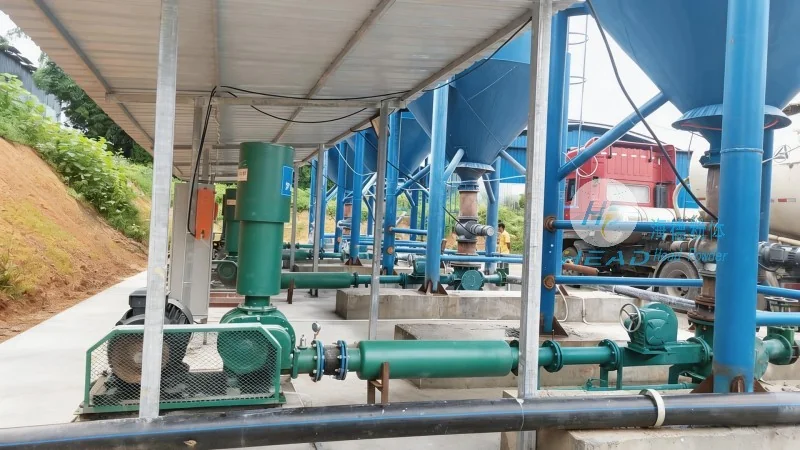
For the special characteristics of phosphate mineral powder, we offer customized pneumatic conveying system solutions. The system uses compressed air or nitrogen as its power source, achieving gas-solid two-phase flow conveying of materials through sealed pipelines. Core equipment includes high-efficiency feeders (such as rotary valves and venturi injectors), wear-resistant conveying pipelines, classification separators, pulse baghouse dust collectors, and intelligent control units. The system can flexibly select positive pressure dilute phase, negative pressure dilute phase, or dense phase conveying modes based on customer site conditions (conveying distance, height difference, output requirements), helping materials flow smoothly in the closed circuit and avoiding dust and external contamination.
Advantages of customized solutions
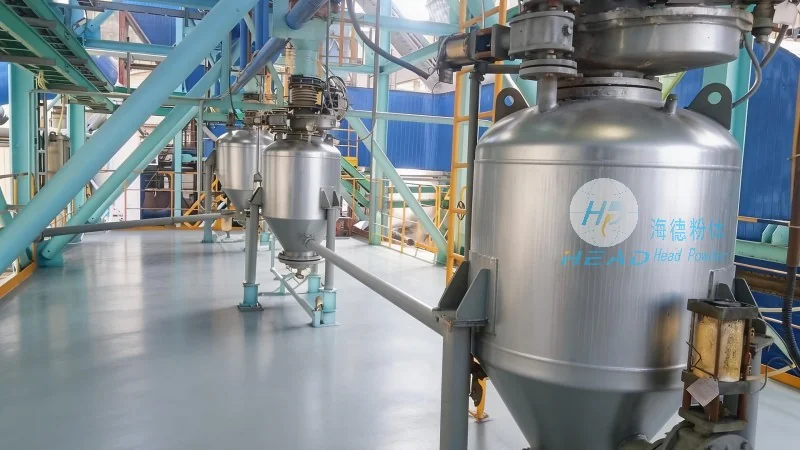
To address customer pain points, we offer the following targeted solutions: using fully enclosed pipelines and high-efficiency dust removal devices to fully eliminate dust leakage and meet environmental protection and occupational health requirements; Wear-resistant elbows and ceramic pipes lined with them reduce wear rates and extend equipment maintenance cycles; Optimized airflow velocity and material-pneumatic ratio design to prevent clogging while reducing energy consumption; Equipped with an automated control system that monitors pressure, flow, and material level in real time, enabling fault warning and remote operation and maintenance, reducing manual intervention and downtime. Ultimately, it helps customers achieve safe, stable, and economical transportation of phosphate ore powder.