

Guiyang rare earth powder inert gas delivery system
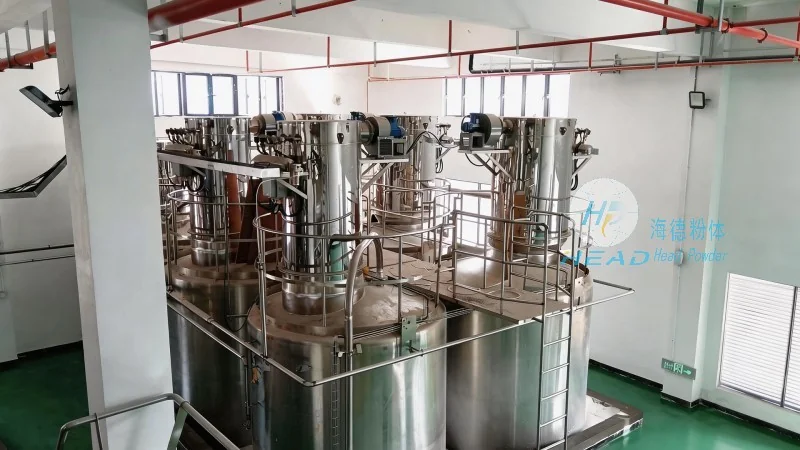
A rare earth materials company has long been engaged in the processing and preparation of rare earth powders at its production base in Guiyang, Guizhou. The company owns multiple powder production lines, but in the powder transportation process, rare earth powders have high chemical activity and are prone to oxidation reactions during conventional air transport, leading to reduced product purity, color deterioration, and safety hazards of dust explosions. Therefore, companies urgently need a reliable sealed conveying system to support powder quality and production safety.
Customer pain points
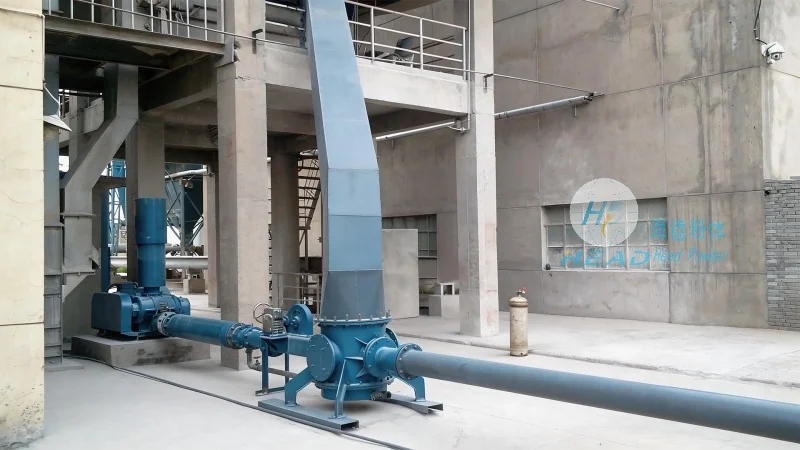
Rare earth powders face the following key issues during transportation: First, after contact with oxygen and moisture in the air, the surface oxidizes rapidly, affecting subsequent sintering and magnetic properties, resulting in unstable batch quality; Second, rare earth powders have fine particle size and low density, which easily generates dust in traditional pneumatic conveying, polluting the environment and increasing material loss; Third, residual oxygen inside the conveying system may ignite the powder, posing an explosion risk; Fourth, existing equipment cannot achieve fully enclosed operation and requires frequent manual cleaning, which affects production efficiency and worker health.
Product advantages
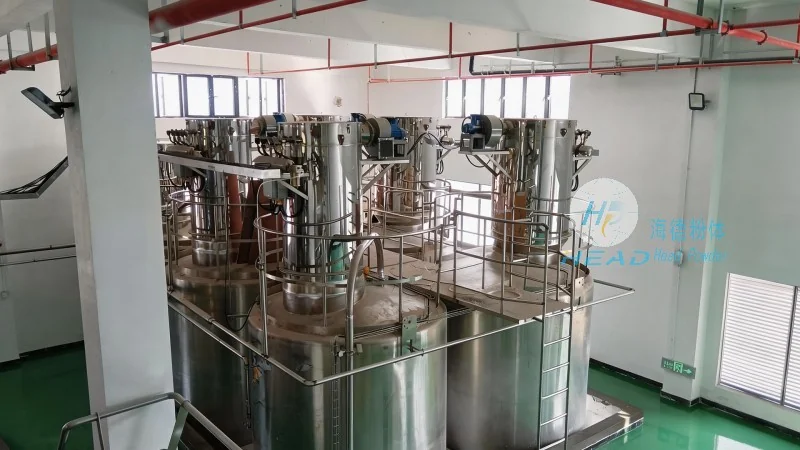
To address these pain points, Head Powder has customized an inert gas delivery system. The system uses high-purity nitrogen as the transport medium, isolating oxygen and moisture from the source and effectively inhibiting rare earth powder oxidation; The pipeline adopts a highly sealed structure, combined with pressure monitoring and automatic replenishment devices to maintain a stable inert atmosphere within the system; Equipped with cyclone separation and bag dust removal modules, achieving efficient gas-solid separation with a material recovery rate exceeding 99.5%; The entire system is automatically controlled by PLC, supporting remote monitoring and parameter adjustment, which reduces the frequency of manual intervention. Through this solution, the company not only improves the consistency of rare earth powder quality but also eliminates the risk of dust explosions, achieving clean, safe, and continuous production.